Cristie L. Preston, Ph.D., CCA
Summary of what you'll find
A dry fertilizer blend is only as good as what comes out of the spreader. What goes into the tender and what lands on the field are not always the same thing.
Segregation, incompatibility, and handling degradation can quietly separate a well-designed blend into its component parts before a single granule reaches the soil. When that happens, the fertility recommendation on paper and the fertility program applied in the field become two different things, and the problem often isn’t recognized until yield maps show uneven nutrient distribution or variable crop performance.
The fertilizer segregation problem
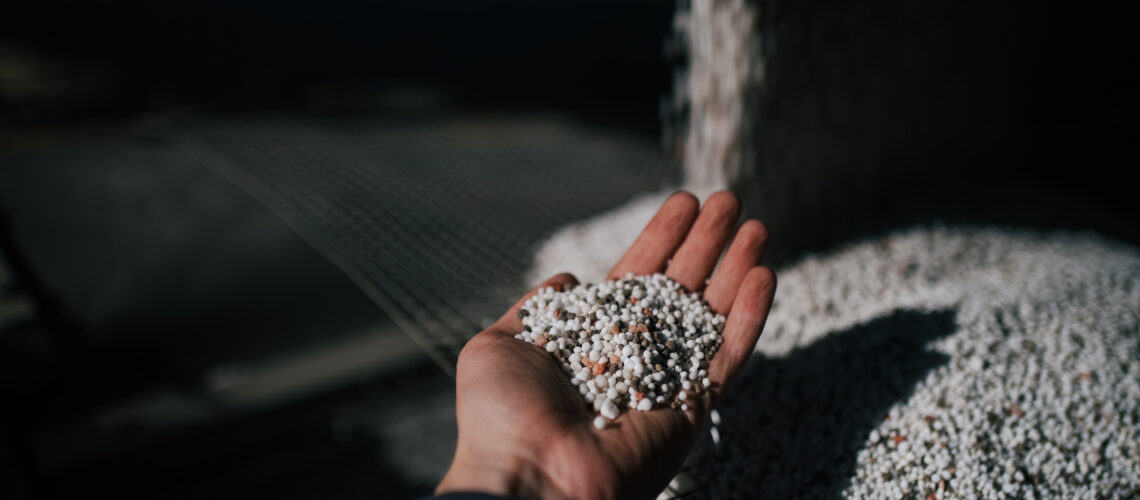
Segregation occurs when the components of a dry blend separate from each other during handling, transport, or application. The primary driver of segregation is a difference in particle size between blend components.
Granules from different fertilizer sources can come in different sizes (also referred to as their SGN value). Dry fertilizer products such as urea, diammonium phosphate (DAP), monoammonium phosphate (MAP), potash, and ammonium sulfate are manufactured to different size specifications. When granules of significantly different sizes are blended, moved, loaded into a tender, conveyed pneumatically, augured into a spreader, or bounced down a gravel road, they separate.
Larger, heavier granules migrate to the outside and bottom of a pile or container, while smaller granules migrate inward and upward. The blend that was uniform when it left the facility is no longer uniform when it hits the spinner. That is not a facility problem; that is a blend specification problem, and it is correctable.
The consequences of fertilizer segregation
The agronomic consequence of segregation is direct. A spreader applying a segregated blend delivers nutrients unevenly across the field – one pass may be heavy in urea and light in potash while the next pass reverses the ratio. While the field averages the right rate on paper, individual plants do not receive the right rate. The result is streaky fields, uneven crop development, and a yield drag that is rarely attributed to its actual cause because the blend wasn’t tested after transport.
The solve to particle segregation in dry blends
The fix to blend segregation is particle size matching. Blend components should be specified to comparable size grades (SGN values within 50 to 75 points of each other are a common industry guideline). Most blend facilities have size data available for their inventory. Asking for size grades before building a blend is a practical step that helps ensure compatible materials are selected for your blend.
Urea-DAP and urea-MAP incompatibility
Chemical incompatibility between urea and phosphate sources is one of the most practically important blend quality issues in the Corn Belt, and one of the least discussed at the grower level.
When urea granules come into contact with DAP or MAP granules in the presence of moisture, a chemical reaction occurs at the granule surface. The reaction produces a sticky product that readily absorbs moisture from the air, causing granules to clump together, absorb additional moisture, and degrade into a caked mass that won’t flow or spread uniformly. The reaction is driven by the pH difference between urea and phosphate sources at the granule surface. The higher the humidity, and the longer the blend sits, the worse the caking becomes.
This matters in practice because urea-DAP and urea-MAP blends are extremely common in Corn Belt fertility programs. A blend built on a dry day in March, stored in a tender over a rainy week, and then applied on a humid April morning is a blend at risk of segregation. Granules that were free flowing when loaded are now potentially clumped and uneven when they reach the spreader, leading to inconsistent application rates. Without knowing it, you’ve degraded nutrient distribution across the field.
Addressing urea-DAP and urea-MAP incompatibility
Management responses include applying urea-phosphate blends as close to the time of blending as possible, avoiding storage of these blends in humid conditions, adding coated or protected urea products that reduce surface reactivity, or substituting liquid phosphate sources for dry phosphate components when blend stability is a priority.
Retailers managing blend inventory through variable spring weather should have a protocol for urea-phosphate blend shelf life to protect blend stability.
Pneumatic conveying and handling degradation
Pneumatic conveyer systems move dry fertilizer efficiently; however, they are also prone to granular degradation.
Every time a granule hits a bend, elbow, or transition point in a pneumatic system at a high velocity, it risks fracturing into smaller particles. Fractured granules behave differently in a blend as they are smaller and lighter. They are also more prone to dust generation, which creates both handling problems and nutrient loss concerns.
Granule hardness varies by product, affecting how well they withstand pneumatic handling. Urea is a relatively soft granule and fractures readily under pneumatic handling stress. Potash granules are harder, while granular ammonium sulfate varies by production method. Some grades are notoriously fragile and degrade visibly after a single pneumatic transfer.
A blend that passes through multiple pneumatic steps, from storage bin to blend plant to tender to spreader, accumulates handling degradation at each step. Depending on the handling system and fertilizer sources, the blend may arrive with a different particle size distribution than when it left the plant. Whether that matters depends on how much degradation occurred and what products were involved.
In practice, consider the full handling chain when specifying blend components. Products that are already near the lower end of their SGN range are more vulnerable to further degradation, and products with known fragility should be handled accordingly or substituted when multiple handling steps are unavoidable.
Hygroscopicity interactions
Some fertilizer materials absorb moisture from the air more aggressively than others. Materials that readily absorb moisture from the air are described as hygroscopic. Urea and ammonium nitrate are both highly hygroscopic, while potash and MAP are relatively stable at moderate humidity. When a blend contains highly hygroscopic components, ambient humidity during storage and handling directly affects blend quality.
Hygroscopic granules that absorb moisture soften, become sticky, and begin to form into a mass, sticking to each other and to container walls. The resulting blend flows poorly, applies unevenly, and may clog spinner mechanisms or conveying equipment. In extreme cases, a blend built with urea and ammonium nitrate components stored overnight in humid conditions arrives at the field as a partially solidified mass that will not spread evenly.
The arithmetic of blend quality failure is straightforward.
A 200-acre corn field receiving an NPK blend that has segregated enough to create a 20 percent variation in nutrient distribution, a level well within the range documented for poorly matched particle size blends, is effectively receiving two different fertility programs simultaneously across that field. The predictability of response to fertilizer at lower soil test levels decreases with this increase in uncertainty. A very common outcome may be the lack of fertilizer responses even when soil tests indicate levels are adequate. The average soil test next fall will look adequate, but the yield map will show variability that is commonly associated with soil type, hybrid placement, or moisture.
Blend quality problems are systematically under-diagnosed because their effects are difficult to isolate, and their cause is rarely tested. Regardless of the fertilizer blend, spreader trucks should be routinely calibrated to ensure proper spreading patterns. Even when your fertilizer blend or single fertilizer applications are assembled correctly, the spreader fan speed could be calculated for a different fertilizer mass. This will also result in non-uniform fertilizer distribution in a field.
A fertility program is only as good as the last step in the delivery chain, and that step is the spreader. Everything before it either preserves the program or compromises it.
Learn more about building quality blends with the following resources:
Sources:
Fertilizer Industry Round Table. 2019. Proceedings of the 69th Annual Meeting.
International Fertilizer Development Center. Fertilizer Manual. 3rd ed. Kluwer Academic Publishers.
Potash & Phosphate Institute. 2001. Soil Fertility Manual.
Mortvedt, J.J., ed. 1999. Micronutrients in Agriculture. 2nd ed. Soil Science Society of America.
TFI (The Fertilizer Institute). Bulk Blending Quality and Handling Guidelines.